Best Master Production Scheduling Software Starts with One Distinction: Master Production Schedule vs Production Schedule
Last updated on : October 14, 2026
Master production schedule vs production schedule sounds like a debate between definitions.
On the shopfloor, it is a delivery question, and the best master production scheduling software has to answer it.
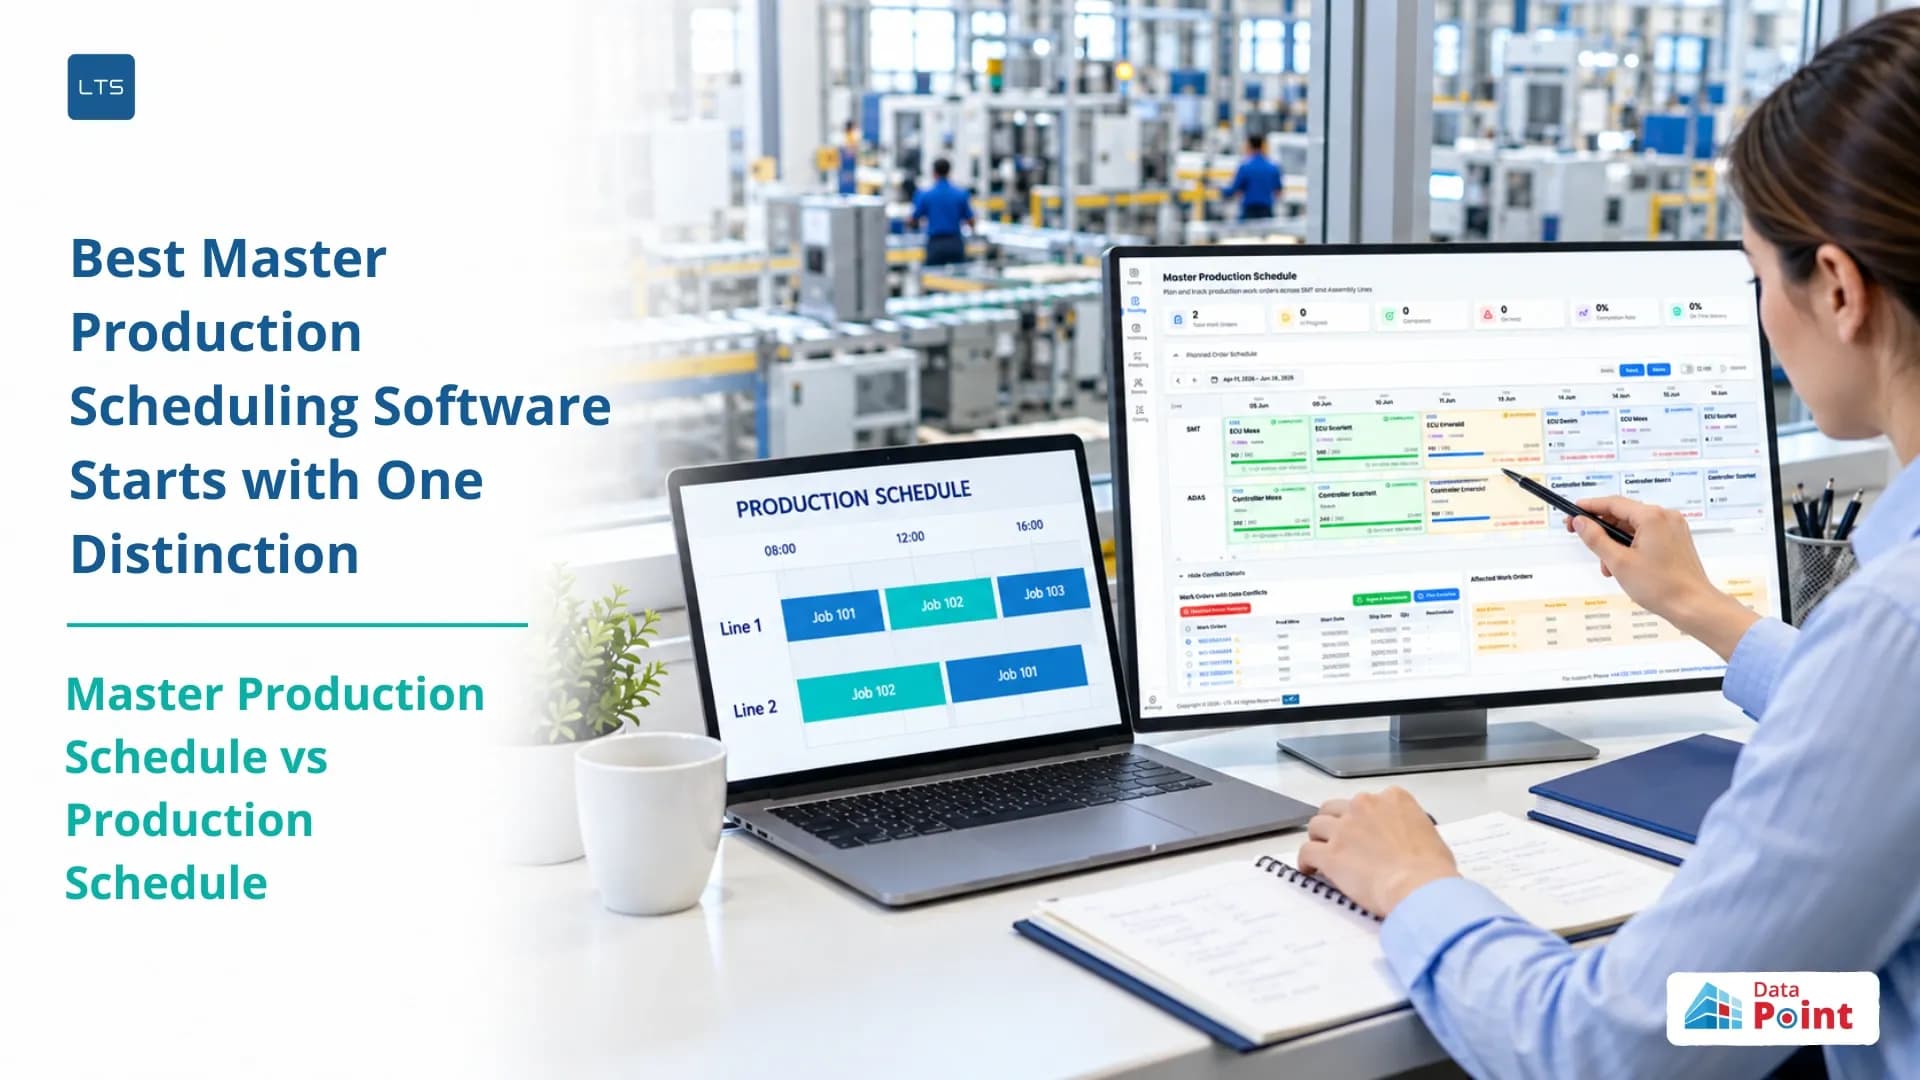
The master production schedule sets what to build, how much and when. Detailed production scheduling then assigns that work to machines, lines and shifts.
Between these two sits an assumption: demand sets the requirement, but it does not confirm the shopfloor can meet it. Material availability, machine capacity and working shifts decide whether the daily production schedule is achievable. When those conditions change without feeding back into planning, the two schedules drift apart.
The gap matters when delivery commitments depend on work the floor cannot complete as scheduled. So how do manufacturers keep the master plan connected to daily execution?
See how LTS Data Point MPS turns ERP demand into a capacity-feasible schedule
Master production schedule vs Production schedule: What each one does
Both schedules check capacity. They check it at very different depths.
The master production schedule works at item level. The production schedule works at job level. The gap between them shows up in four places:
- Level of detail: The master schedule sets items, quantities and dates by period. The production schedule sets individual jobs with start and finish times.
- Capacity check: The master schedule takes a rough-cut view of key resources. The production schedule checks capacity job by job.
- Time horizon: The master schedule looks weeks ahead and beyond. The production schedule looks days and shifts ahead.
- Owner: The master schedule sits with planning. The production schedule sits with production control or the shopfloor planner.
Rough-cut capacity planning shows how this works in practice. It converts the master schedule into a view of required and available capacity at key resources, such as bottleneck work centres, before the plan is implemented. That confirms the plan is possible. It says little about how Tuesday’s second shift will run it.
How the master schedule becomes the daily production schedule
The handover is where the plan meets the floor. At one beverage producer, the weekly master schedule is chosen in a planning system. Its volumes then load into a scheduling system, which generates production orders to fit batch sizes and sequences them to cut setups on the filling line. Weekly quantities become orders. Orders become sequenced jobs. Skip that second step and the first is a wish list.
Picture a weekly plan that clears the rough-cut check. On Tuesday, a changeover overruns by two hours. The sequence built around it slips, and by mid-shift the line is running a different order from the one on paper.
A rough-cut check shows the plan is possible, not that the shift will deliver it. So, what changes in between?
Why the master plan and the daily schedule drift apart
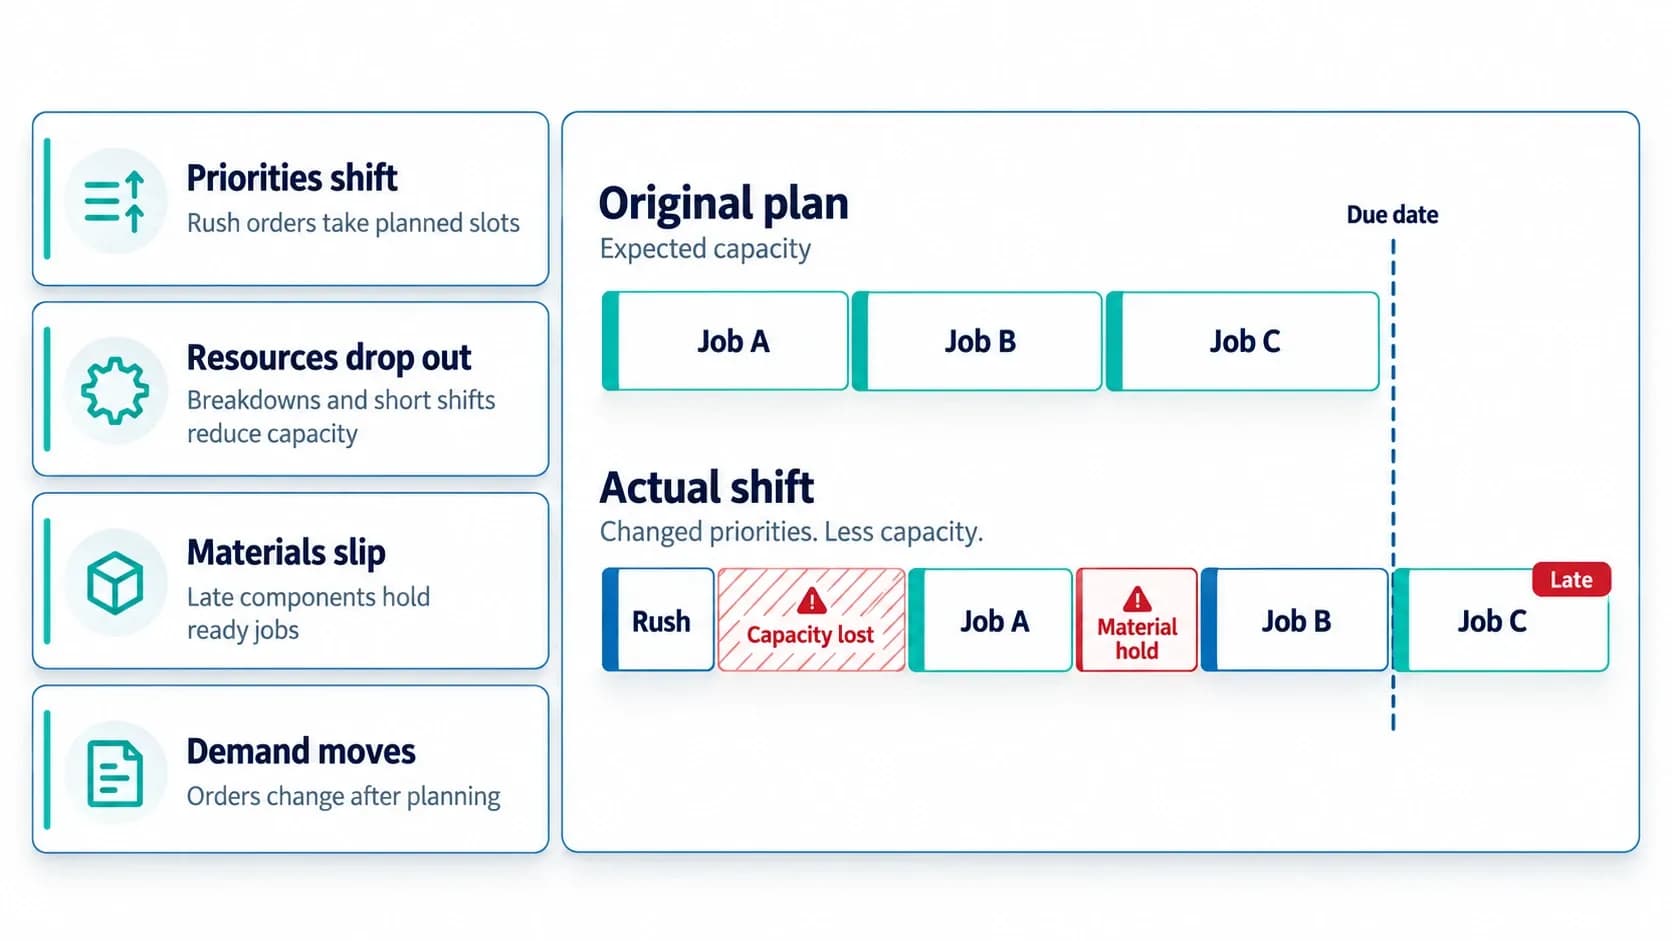
A schedule is only as realistic as the capacity behind it. At one UK automotive electronics plant, the ERP held demand and MRP planning. Capacity-aware scheduling, OEE-adjusted minutes and shift visibility had to come from elsewhere. Without that view, a plan assumes full capacity. The floor has less.
Production scheduling constraints decide what can run today. Production capacity constraints cap how much. Both move once the plan is set.
Four things change between the plan and the shift:
- Priorities shift. A rush order takes the slot another order held.
- Resources drop out. A machine goes down or a shift runs short, and capacity shrinks.
- Materials slip. A late component holds a job that was ready to run.
- Demand moves. Orders are added, changed or cancelled after the schedule is set.
Researchers have put a number on one such event. In a simulated three-line feed plant, two machines failed at the same moment. Total completion slipped from 76 to between 80 and 87 time units, depending on the rescheduling method. Some jobs finished up to 48 units late.
Overloaded lines. Missed due dates. Expediting that pushes other orders back.
The plan was not wrong when it was made, but it stopped being true on the floor. So how does a planner see the slip before the due date does?
How to spot and close the gap between plan and actual
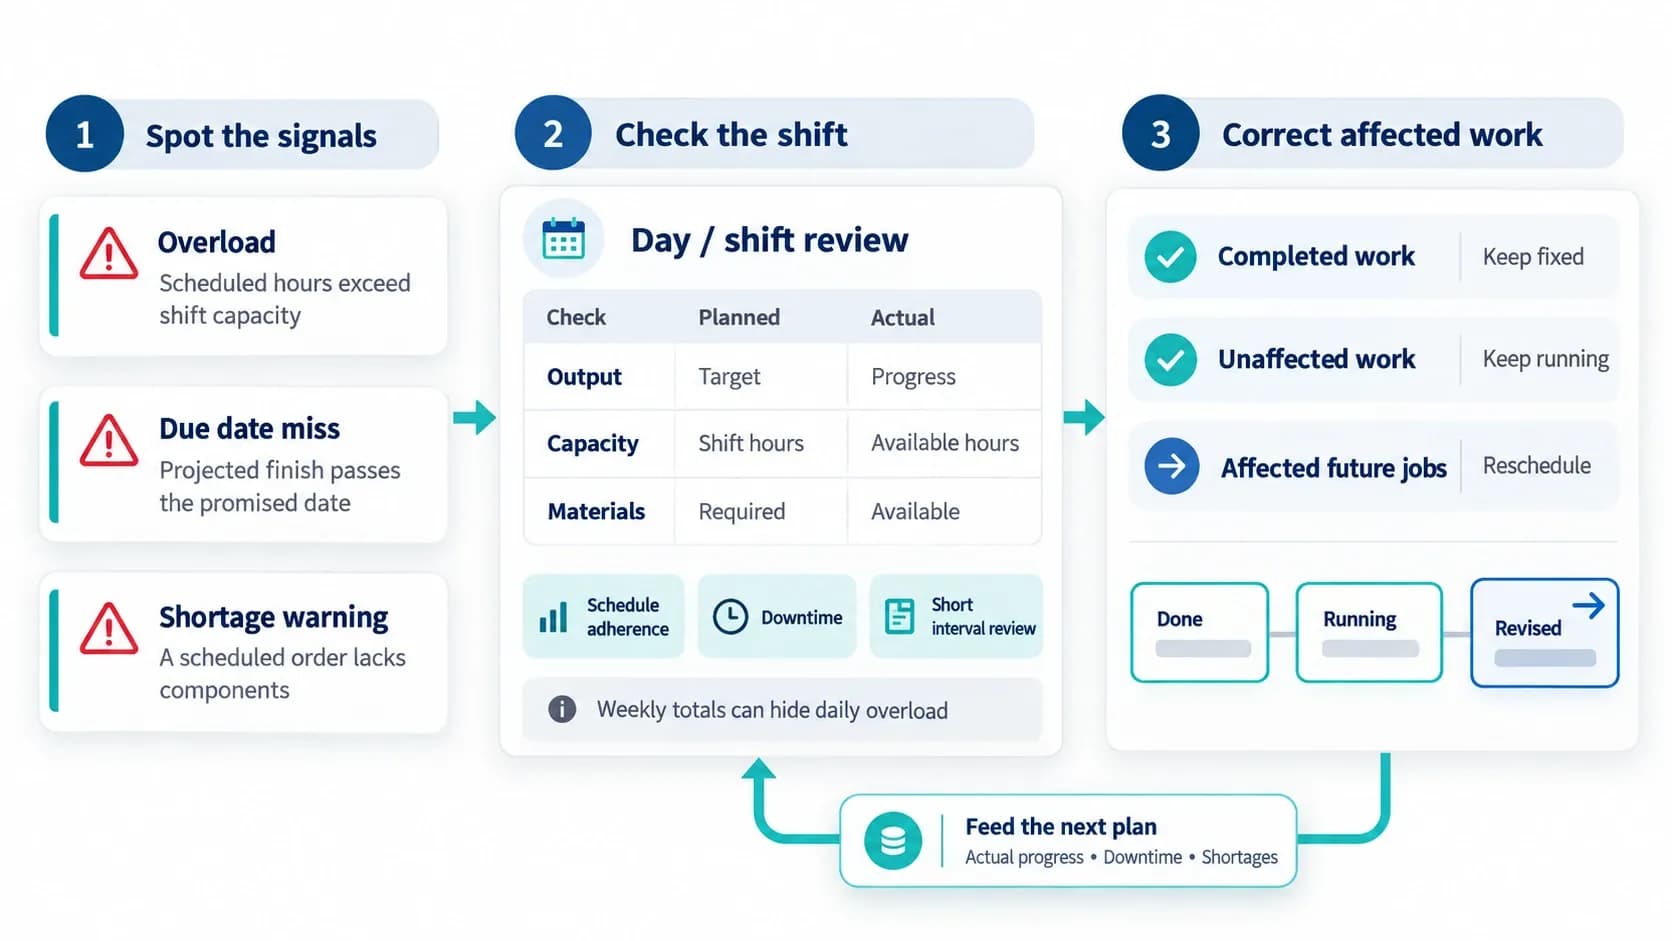
The gap rarely announces itself. It shows up as small signals long before a due date slips.
Three signals show a schedule is drifting:
- Overload. A line or work centre carries more hours than the shift can supply.
- Due date miss. A job’s finish date now falls after the date promised, and delivery KPIs start to slip.
- Shortage warning. A component is late or short for an order already scheduled.
Each signal is a comparison. Scheduled work sits on one side. Actual progress sits on the other. Planned vs actual production is the first check. Production schedule adherence goes further. It measures how closely actual jobs, quantities and timing follow the schedule. Read at every review, it shows production delays while they are still small. An OEE tracker adds the downtime behind any gap, and a short interval control board puts the comparison in front of the team during the shift.
The level of the check matters. One planning system’s documentation shows why. In a weekly bucket, a resource can be overloaded on some days and still raise no overload exception, as long as the week’s total capacity is enough. A quiet screen can hide a loaded line. Only a day and shift view shows it.
One signal rarely touches one order. In one manufacturing system, a single component shortage can be linked to all three work orders that use it, and supervisors are notified. The correction can stay just as narrow. In one 2025 study, finished jobs stay untouched when a machine fails. Work on running machines continues as planned, and only later scheduling is adjusted. That is the standard to aim for: a small, fast correction, not a full rebuild.
Closing the gap works the same way. Actual progress, downtime and shortages go back into planning. Production plan vs actual output then shapes the next plan, and keeping production schedules aligned becomes routine, not a rescue.
The gap itself is normal. Leaving it unseen is the failure. So, what does it take to see it, and close it, in one place?
How LTS Data Point MPS connects the master plan to daily execution
The best master production scheduling software closes the gap in one place. LTS Data Point MPS sits between the ERP and the shopfloor and turns the master plan into a schedule the floor can run. Three capabilities make that work:
- Demand becomes a feasible schedule. Planned orders come in from the ERP integration. Data Point MPS schedules them onto work centres using routing-based durations and OEE-aware capacity.
- Conflicts reach the planner first. Blockers and warnings show before the plan reaches the line.
- The loop closes. Production records and declarations flow back to the ERP, so the schedule and the ERP see what the floor delivered.
The ERP keeps MRP and order creation. Shift management software holds the working pattern, Data Point MPS schedules the demand it receives, shift by shift. At one UK plant, planned orders synchronise from the ERP and are scheduled by drag and drop, then checked in a capacity view and a calendar view. The daily production schedule rests on capacity the floor can supply, so unrealistic production schedules are caught at the desk.
Blockers, such as a missing routing or cycle time, hold an order back until the data is fixed. Warnings, such as overload, a due date miss or a material shortage, stay visible for the planner to resolve. Those are the same three signals that show a schedule drifting, now caught before the floor feels them. Production scheduling conflicts get resolved at the desk, not on the line.
The planner reviews the proposed schedule and decides what to commit. Production records and finished-goods declarations flow back to the ERP, and performance and capacity reports sit beside the planning report. That feedback keeps the master plan and the daily schedule aligned.
Around the schedule sits the scorecard. Data Point AI works inside it. It monitors KPI trends and flags a slipping delivery score before it crosses a threshold. Every recommendation stays a suggestion. A person approves the action, the same principle as the planner commit step.
The master plan sets the target. The shopfloor delivers it. Data Point MPS and Data Point AI connect the two on one platform.
The master production schedule sets the target. The production schedule decides whether the floor can hit it. When conditions change, the two drift apart. Early signals and small corrections keep them aligned. Data Point MPS keeps both in one view, so the plan stays a promise the floor can keep, not hope.
Call an LTS Data Point expert to talk through connecting your master plan to daily shopfloor scheduling
FAQs
1. Is a master production schedule the same as MRP?
No. A master production schedule sets the quantities and timing of planned production. Material requirements planning (MRP) uses those requirements, bills of materials and inventory information to calculate which components are needed and when.
2. Can manufacturers use a master production schedule for make-to-order production?
Yes. An MPS can use confirmed customer orders as well as forecasts. In make-to-order manufacturing, the balance depends on the products, lead times and how much production is triggered by individual orders.
3. Does every change to the daily production schedule require an MPS update?
Not necessarily. Moving jobs between machines or shifts may leave planned product quantities and completion dates unchanged. Review the MPS when a change affects those requirements or the capacity needed to fulfil them.
4. What is a frozen period in a master production schedule?
A frozen period is a near-term window in which schedule changes are restricted or tightly controlled. It helps protect committed materials, resources and work from frequent changes. Its length depends on the operation’s lead times and flexibility.
5. Can Excel handle master production scheduling?
Excel can support a simple MPS when volumes, constraints and changes are manageable. The challenge grows when several planners need to coordinate shared resources, maintain current data and assess the effect of changes across orders.
6. Is production schedule adherence the same as on-time delivery?
No. Production schedule adherence measures whether work follows the agreed schedule. On-time delivery measures whether the customer receives the order by the agreed date. A plant can recover from a schedule deviation and still deliver on time.
7. What should manufacturers look for in master production scheduling software?
Look for capacity-feasible scheduling built on routings and OEE-aware capacity, conflicts shown to the planner before the plan reaches the floor, and production feedback flowing back to the ERP. Check how it connects to your ERP and whether the planner approves each commit.